Last Updated: October 23, 2026
Quick Summary
Hiring for CNC and quality inspection works when you define the roles separately, test skills before the interview, and set pay and schedule expectations before posting. Post CNC operator, CNC machinist, and quality inspector as distinct roles, screen with a practical assessment and blueprint reading test, and publish a pay range built from local market data.
- Post CNC operator, CNC machinist, and quality inspector separately unless you have a specific reason not to.
- A blueprint reading test should take under 20 minutes and use a real print from your shop.
- Set pay from local market data and publish the range so candidates do not skip your listing.
- A common hiring cycle runs two weeks from application to offer, with a decision within 48 hours of the last step.
- Build the first 30 days around safety, supervised measurement, nonconformance handling, and an independent audit.
Table of Contents
- Hiring for CNC and Quality Inspection: Why the Process Breaks Down
- Define the Roles Before You Post the Job
- CNC Machinist Skills Assessment: What to Test and How
- The Blueprint Reading Test for Machinists That Actually Filters Candidates
- Quality Control Inspector Interview Questions Worth Asking
- Manufacturing Hiring Best Practices for Pay, Shifts, and Time-to-Fill
- Onboarding and Retention: Keeping the Hires You Just Made
- Conclusion
- Frequently Asked Questions
Hiring for CNC and Quality Inspection: Why the Process Breaks Down
Hiring for CNC and quality inspection fails for one reason: most shops post a single vague job description and hope the right person walks in, flooding the inbox with unqualified resumes and stretching time-to-fill until production suffers. IntegrityJobs has 30 years of experience placing technical talent across Ohio’s manufacturing sector, and the shops that hire well often define the role precisely, test skills before the interview, and set pay ranges that reflect the actual market.
The stakes are higher than most hiring managers admit. A bad CNC hire wastes training hours, creates scrap, and disrupts a shift. A bad quality inspector hire is worse: nonconforming parts can reach a customer and trigger a recall.
Define the Roles Before You Post the Job
The fastest way to waste a hiring cycle is to blur three distinct jobs into one posting. CNC operator, CNC machinist, and quality inspector require different skills, pay bands, and screening methods. Post them separately unless you have a specific reason not to.
CNC Operator vs. CNC Machinist vs. Quality Inspector
A CNC operator loads material, runs an established program, monitors the machine, and checks parts against a defined standard, following a setup someone else created.
A CNC machinist does everything an operator does, plus setup, tool selection, offset adjustment, and often programming. Machinists read blueprints, interpret tolerances, and troubleshoot out-of-spec parts.
A quality inspector works the other side of the process, verifying completed parts against inspection requirements, measuring dimensions with metrology tools, documenting results, and flagging nonconforming parts before they ship.
| Role | Core Responsibility | Typical Experience | Key Skill Tested |
|---|---|---|---|
| CNC Operator | Run established programs, monitor output | Entry to 2 years | Machine safety, in-process checks |
| CNC Machinist | Setup, offsets, programming, troubleshooting | 3-7 years | Blueprint reading, GD&T, setup |
| Quality Inspector | Measure, document, disposition parts | 2-5 years | Metrology, traceability, standards |
When One Hire Needs Both Skill Sets
Some shops genuinely need a quality control machinist, someone who runs the machine and inspects their own output to a documented standard. This works in small shops where volume is low and one person owns a part from stock to shipping.
The risk is real, though. Asking one person to both produce and inspect removes the independent check that catches defects. If you go this route, build in a second-party audit at final inspection.
Combining production and inspection into one role saves headcount but weakens your quality system. If a customer audit or an aerospace contract requires independent verification, a self-inspection setup can cost you the account.
CNC Machinist Skills Assessment: What to Test and How
Test skills before the interview, not during it. A structured assessment filters out candidates who interview well but cannot read a tolerance or set an offset.
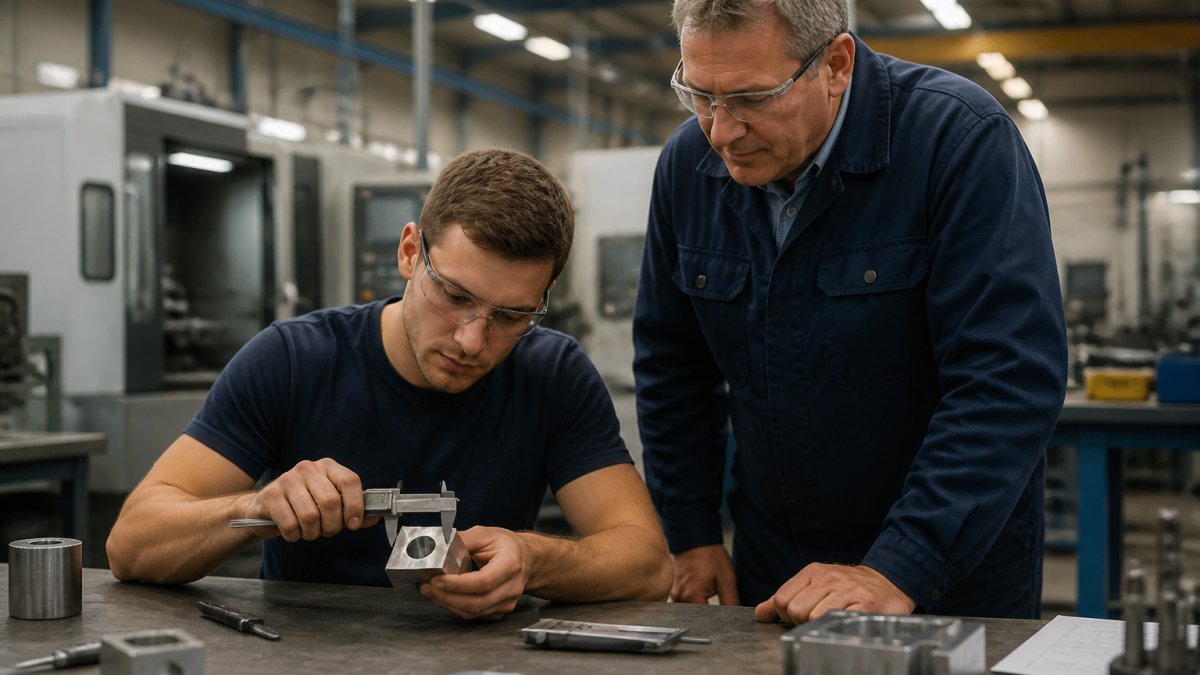
Start with a short practical screen: give candidates a sample part and a print, then ask them to measure three features and state whether each passes. Fifteen minutes tells you more than an hour of conversation.
Metrology Tools and Technical Competencies to Verify
A machinist who cannot use measuring tools correctly is a liability. Verify hands-on familiarity with the instruments your shop actually uses:
- Calipers for outside, inside, and depth measurements
- Micrometers for precise outside diameters
- Height gauges for feature location from a datum
Ask the candidate to zero a micrometer and read a known standard. Trusting a digital readout without checking the tool against a standard is a common mistake, catch it in the assessment, not on the floor.
The Blueprint Reading Test for Machinists That Actually Filters Candidates
A blueprint reading test for machinists should take under 20 minutes and use a real print from your shop, redacted as needed, with a mix of tolerances, datums, and at least one geometric dimensioning and tolerancing callout. Then ask four questions:
- What is the nominal dimension and its tolerance on the critical feature?
- Which datum controls the location of this hole?
- Does this feature pass or fail as measured?
- What would you adjust if the part ran oversize?
Score each answer pass or fail. Candidates who cannot answer questions 1 and 2 are not ready for a machinist role, regardless of years listed on the resume. The National Institute for Metalworking Skills publishes credential standards that give you a benchmark for what a machinist should know at each level.
Use a print from a job your shop actually runs. Generic textbook prints miss the specific tolerances, materials, and callouts your machinists handle daily, so they filter for the wrong skills.
Quality Control Inspector Interview Questions Worth Asking
The best quality control inspector interview questions probe how a candidate thinks when a part is borderline.
Ask these directly and listen for specifics:
- Walk me through how you handle a part that measures at the tolerance limit.
- How do you document a nonconforming part, and who do you notify?
- What do you do when a gauge reads differently than expected?
Strong answers reference a documented process: quarantine the part, record the measurement, notify the supervisor, and follow the disposition procedure. Weak answers improvise.
The American Society for Quality maintains certification standards for quality inspectors that give you a reference point for expected competencies, including calibration, sampling, and inspection planning.
Manufacturing Hiring Best Practices for Pay, Shifts, and Time-to-Fill
Manufacturing hiring best practices come down to three levers: competitive pay, clear shift expectations, and a fast process. Get any one wrong and your best candidates take another offer. Skilled machinists and inspectors often have two or three options, and the shop that moves first usually wins.
Post the shift and schedule up front. First shift, Monday through Friday, is the most requested and hardest to fill from a standing start. If the role requires rotating shifts or weekends, say so, candidates who discover the schedule late drop out and you restart the search.
Setting Pay Ranges That Compete
Set your pay range from local market data, not what you paid the last person. Define a floor for entry, a midpoint for proven machinists, and a ceiling for candidates who can program and inspect.
Build the range in four steps so it survives a candidate conversation and a budget review:
- Pull local data, not national averages. Use Bureau of Labor Statistics Occupational Employment and Wage Statistics for the relevant occupation and area, plus current postings in your commuting radius. National averages overstate pay in rural areas and understate it in tight industrial markets.
- Separate the bands by skill, not title. An operator who loads and monitors is a different band from a machinist who sets up, adjusts offsets, and edits programs, and both differ from an inspector who dispositions nonconforming parts. One band for three skill levels guarantees you lose the top of the market.
- Price the shift differential explicitly. Second and third shift typically carry a premium, and a rotating schedule carries a larger one. State the differential in dollars per hour in the posting so candidates compare total pay, not base rate.
- Decide the ceiling before the interview. Know the top of your range and what justifies it, programming, CMM operation, GD&T fluency, or a certification, so the offer is a decision, not a negotiation from scratch.
Publish the range as a band with the factors that move a candidate within it. “$22-$30 per hour depending on setup, programming, and inspection experience” tells a strong candidate where they land and a weak one they will not clear the midpoint.
Shift Structures That Actually Fill
Most shops run one of four patterns, and each has a different hiring cost:
- Straight first shift, Monday through Friday. Easiest to fill, shortest time-to-fill, and the pattern most experienced machinists and inspectors prefer.
- Straight second or third shift. Fills slower and requires a differential, but retains well once someone settles into the schedule.
- Rotating shifts. The hardest to fill and the highest turnover risk; if you use it, say so in the first line of the posting and price the premium accordingly.
Compressing Time-to-Fill
A slow process loses good candidates regardless of pay. A common pattern is a two-week cycle from application to offer: a same-week phone screen, a scheduled practical assessment, one panel interview, and a decision within 48 hours of the last step.
The three levers that decide whether you fill a CNC or inspection role are pay transparency, schedule clarity, and speed. Fix all three before you post, and your time-to-fill drops.
If you need someone in three to four weeks and your internal pipeline is thin, a specialized staffing partner can shorten the search. IntegrityJobs maintains a vetted pool of machinists, inspectors, and technicians across all 88 Ohio counties.
Onboarding and Retention: Keeping the Hires You Just Made
Retention starts on day one, not at the 90-day review. A new machinist or inspector dropped into a shift without a plan starts looking within weeks.
For a regulated manufacturer, onboarding a quality inspector or a machinist who performs in-process inspection is a qualification process, not an orientation. Build the first 30 days around the competencies the role must demonstrate before the person signs off on a part unsupervised.
A 30-Day Onboarding Sequence for CNC and Inspection Hires
Week 2, Supervised measurement and documentation. The hire measures parts under supervision and completes inspection records, including lot or serial traceability.
Week 3, Nonconformance handling. Walk through a real or simulated nonconforming part: quarantine, measurement record, notification, disposition, and corrective action.
Week 4, Independent work with audit. The hire works independently while a second party audits a sample of their inspections.
Calibration, Traceability, and the Documents New Hires Must Know
Point every new inspector and machinist to the specific documents behind their daily work:
- Inspection plan, which features are measured, with what instrument, at what frequency, and to what tolerance.
- Calibration records, how to confirm a gauge is in calibration before use, and what to do when a gauge is out or reads unexpectedly.
- Traceability records, how a measurement ties back to a lot, serial number, or work order so a defect can be contained if it surfaces later.
For the compliance side, point new inspectors to the International Organization for Standardization’s quality management standards so they understand the traceability and documentation expectations behind their daily work. If your customers require it, also orient them to the American Society for Quality certification framework as a development path.
Retention Levers That Matter After Week Four
Contract-to-hire placements fail when the fit is wrong, not when the skills are wrong. Screen for shift compatibility and team fit during the interview, and set clear expectations about the conversion timeline.
Beyond fit, the levers that keep machinists and inspectors are predictable: a clear path from operator to machinist to lead, pay progression tied to demonstrated skill rather than tenure, and a schedule that does not change without notice.
Track a 30-60-90 check-in cadence and review the new hire’s inspection records at each point. Documentation quality is the earliest signal of whether an inspector is ready for independent sign-off.
Conclusion
Filling a CNC or quality inspection role is a process problem, not a luck problem. Define the role, test the skills, ask the questions that expose how a candidate thinks, and set pay and schedule expectations before you post.
If your shop needs vetted machinists and inspectors without the drawn-out search, IntegrityJobs can help. We bring 30 years of technical recruiting experience, a woman-owned approach built on fairness and speed, and flexible contract-to-hire options.
Frequently Asked Questions
What is the difference between a CNC operator and a CNC machinist?
A CNC operator runs a machine that is already set up: loading parts, checking output, and flagging problems. A CNC machinist owns more of the process, including setup, tool changes, offsets, and often programming. For hiring for CNC and quality inspection, this distinction sets your screening bar. Operators can be assessed on throughput and inspection discipline; machinists should be tested on setup decisions, tolerance interpretation, and troubleshooting. Pay reflects the gap, so write the job title to match the actual work or you will attract the wrong candidates.
How do you assess a CNC machinist’s skills during an interview?
Use a two-part CNC machinist skills assessment. First, a short practical task: give the candidate a print with tight tolerances and ask which tools and setup they would use, then have them measure a sample part with calipers and a micrometer. Second, behavioral questions about scrap, offsets, and machine alarms. Ask them to walk through a time they caught a nonconforming part before it shipped. Candidates with real experience answer with specifics: which instrument, which tolerance, what they changed. Vague answers are your signal to keep looking.
How can employers test a candidate’s blueprint-reading skills?
A blueprint reading test for machinists should take 15 to 20 minutes and use a real print from your shop, redacted as needed. Ask the candidate to identify datum features, interpret GD&T callouts, find the tightest tolerance on the drawing, and state which measurement tool they would use for each critical dimension. Score answers on correctness, not speed. You can also hand them a completed part and the matching print and ask them to verify two dimensions. This shows whether they can connect the drawing to the physical part, which is the skill that prevents nonconforming parts from shipping.
How long does it take to hire a CNC machinist or quality inspector?
Timelines vary by market and skill level, but the steps that slow most shops down are posting approval, interview scheduling, and background checks. Compress each one: approve the pay range before posting, batch interviews into two days, and start screening the same week you post. Working with a staffing partner can shorten the front end because vetted candidates are already in the pipeline. IntegrityJobs, with 30 years placing technical talent, can discuss realistic timelines for your area when you contact them.